SP-1000 Special-Purpose Machining Center for Batch Automotive & Motor Parts
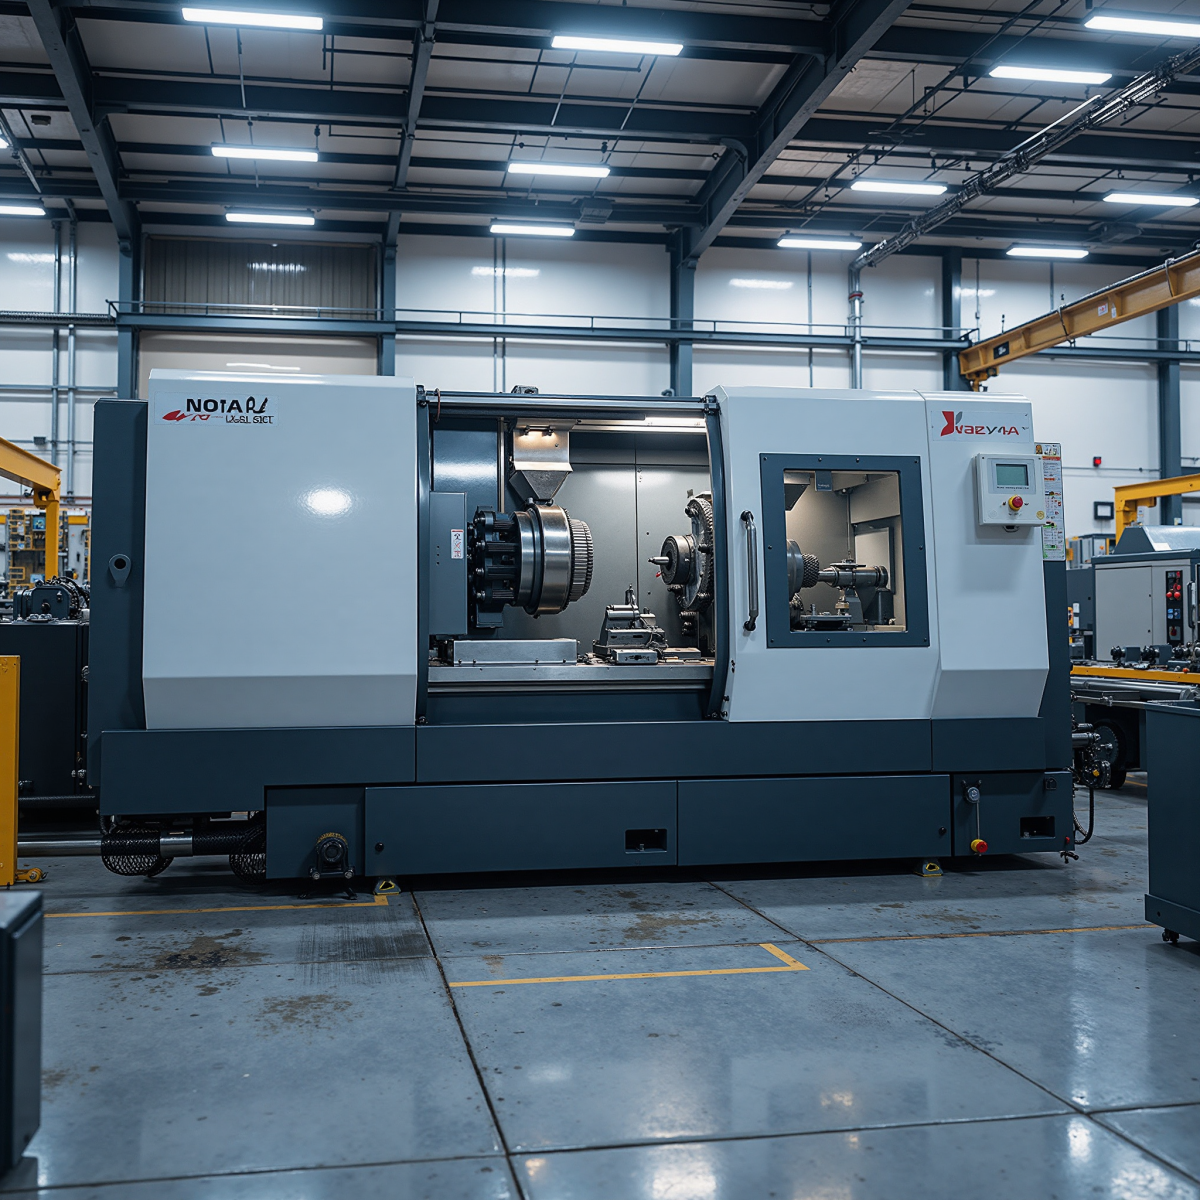
A special-purpose machine concept built around automotive brackets, housings and motor parts. Instead of a general-purpose envelope, the fixture, spindle orientation and tooling are configured to the specific part family so that batch takt time and consistency improve.
- CategorySpecial-Purpose Machine
- dual-station unit for automotive bracket batch machiningSP-1000-AUTO
- dedicated unit for motor housings and end capsSP-1000-MOTOR
- rotary-index version for multi-face parts with auto loadingSP-1000-ROTARY
Price and lead time are quoted per configuration and quantity. Send us your part or capacity requirement and we will come back with a quotation.
Designed Around a Part Family, Not a Catalogue Envelope
The SP-1000 is not a general-purpose machining center. Its stroke, fixture and spindle layout are configured to one family of parts, for example automotive brackets and covers or motor housings and end caps, so that clamping is repeatable and the cutting path is short.
Machine Layout and Workstations
Depending on the part, the machine may be laid out as a single-station unit with a trunnion, a dual-station unit alternating load and cut, or a rotary-index configuration for multi-face parts. Each layout is chosen to keep the operator cycle outside the cutting time.
Key Specifications Overview
| Item | Typical parameter |
|---|---|
| Configuration | single-station, dual-station or rotary-index |
| Spindle taper | BT40 / BT50 (selected to the part) |
| Spindle speed | up to 8000 r/min |
| Tool magazine | 8–24 stations, part-dependent |
| Clamping | dedicated hydraulic / pneumatic fixture |
| Positioning accuracy | to the tolerance of the key features |
| Control | mainstream CNC, handshake with line PLC |
Fixtures, Tooling and Tool Change
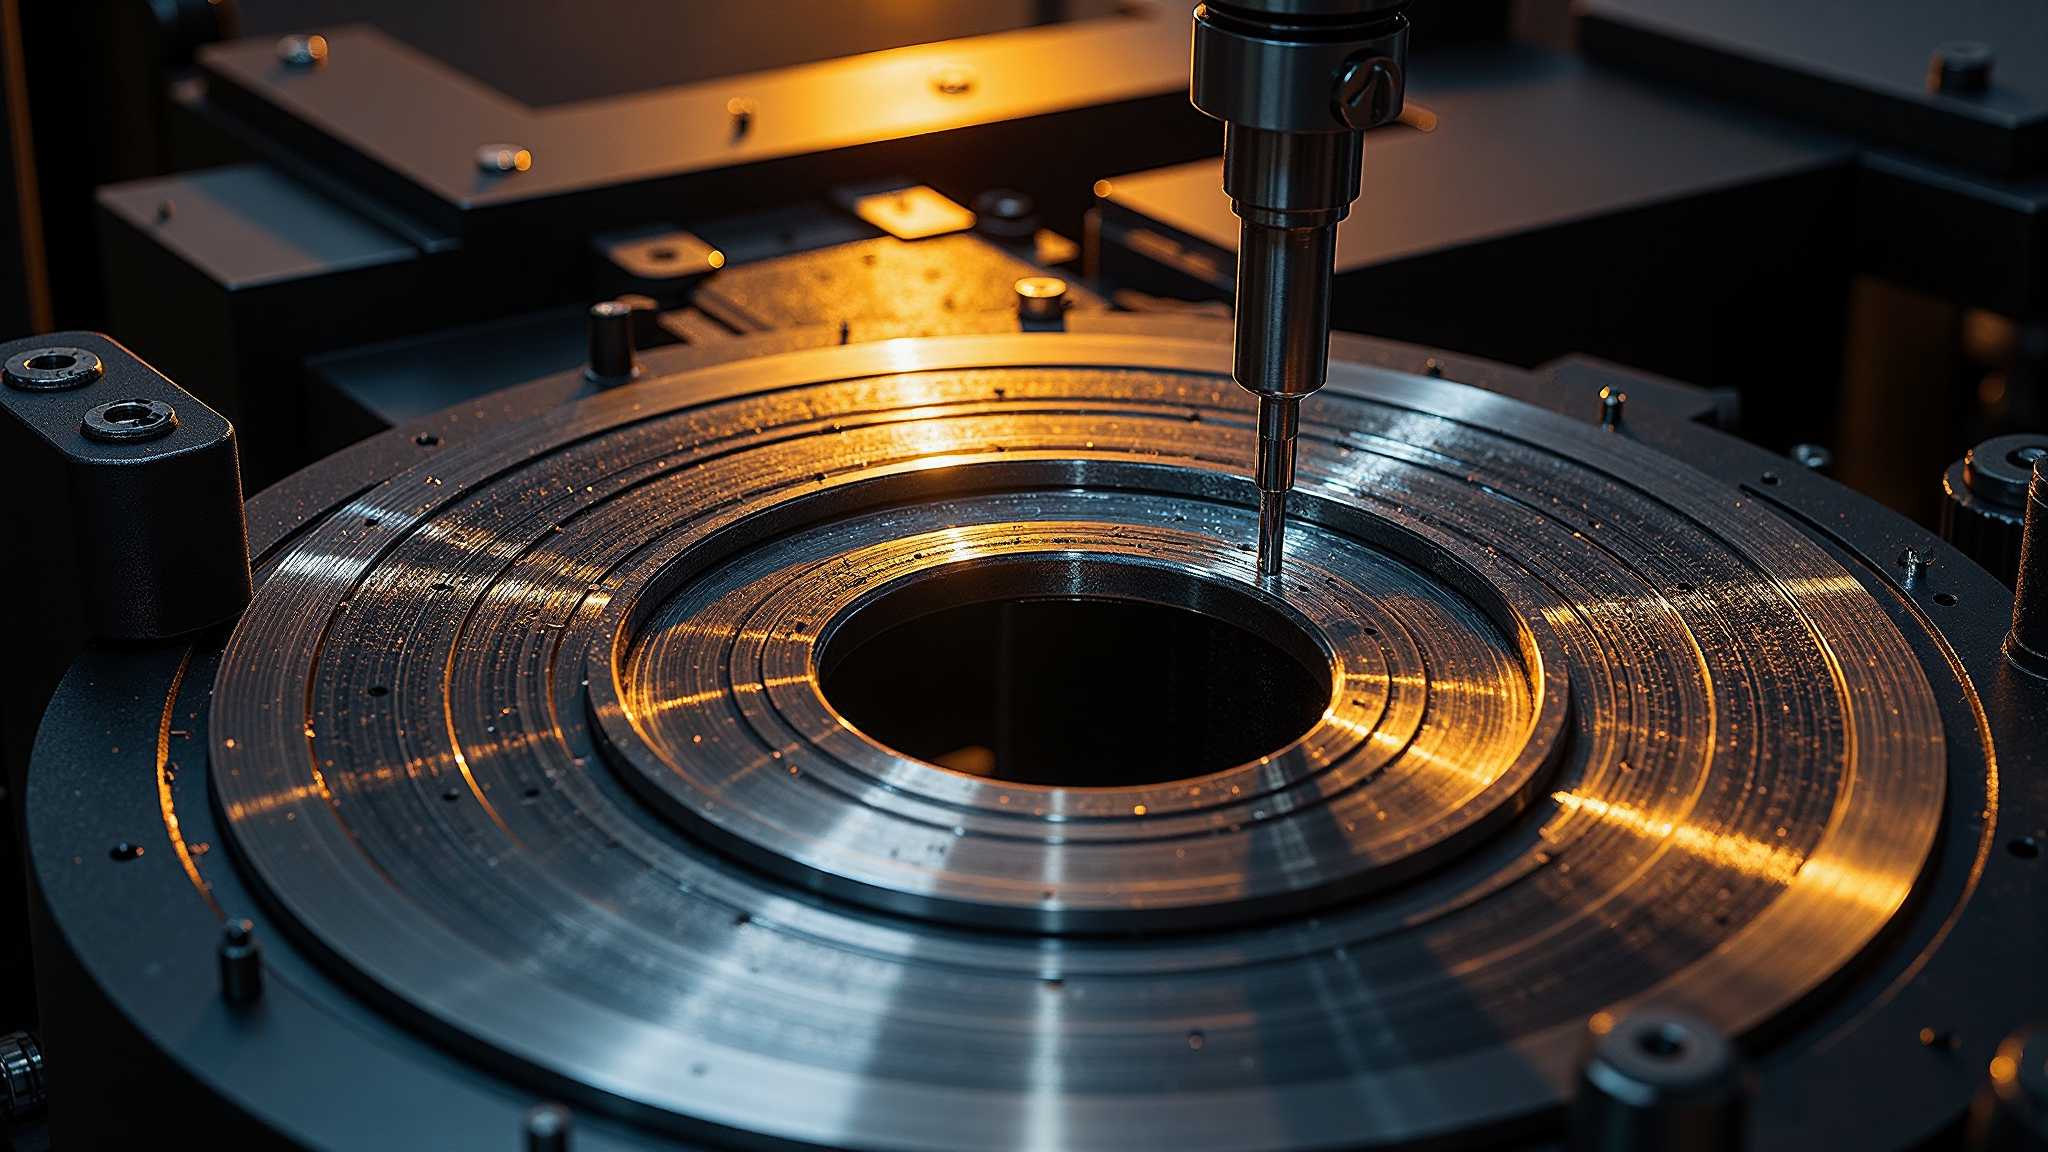
Dedicated fixtures are designed together with the process so that location and clamping repeat exactly from part to part. Tooling is grouped by feature, which reduces the number of tool changes within one cycle.
Automation and Line Integration
The machine can be fitted with an automatic loading arm, a gantry loader or a robot interface, and it can handshake with a production line PLC so that loading, machining and inspection are coordinated.
Configuration and Acceptance Points
Describe the exact part drawing, annual volume and required takt, then agree on the fixture concept, the key tolerances and the acceptance method (gauges or CMM). Acceptance usually includes a trial run of the agreed batch and a check of the critical dimensions. Final configuration and quotation are subject to inquiry confirmation.
Need a Different Configuration?
Tell us the parts you machine and the batch size — we will recommend a machine or process that fits.