PM-6500 Profile Machining Center for Long Aluminum Profiles
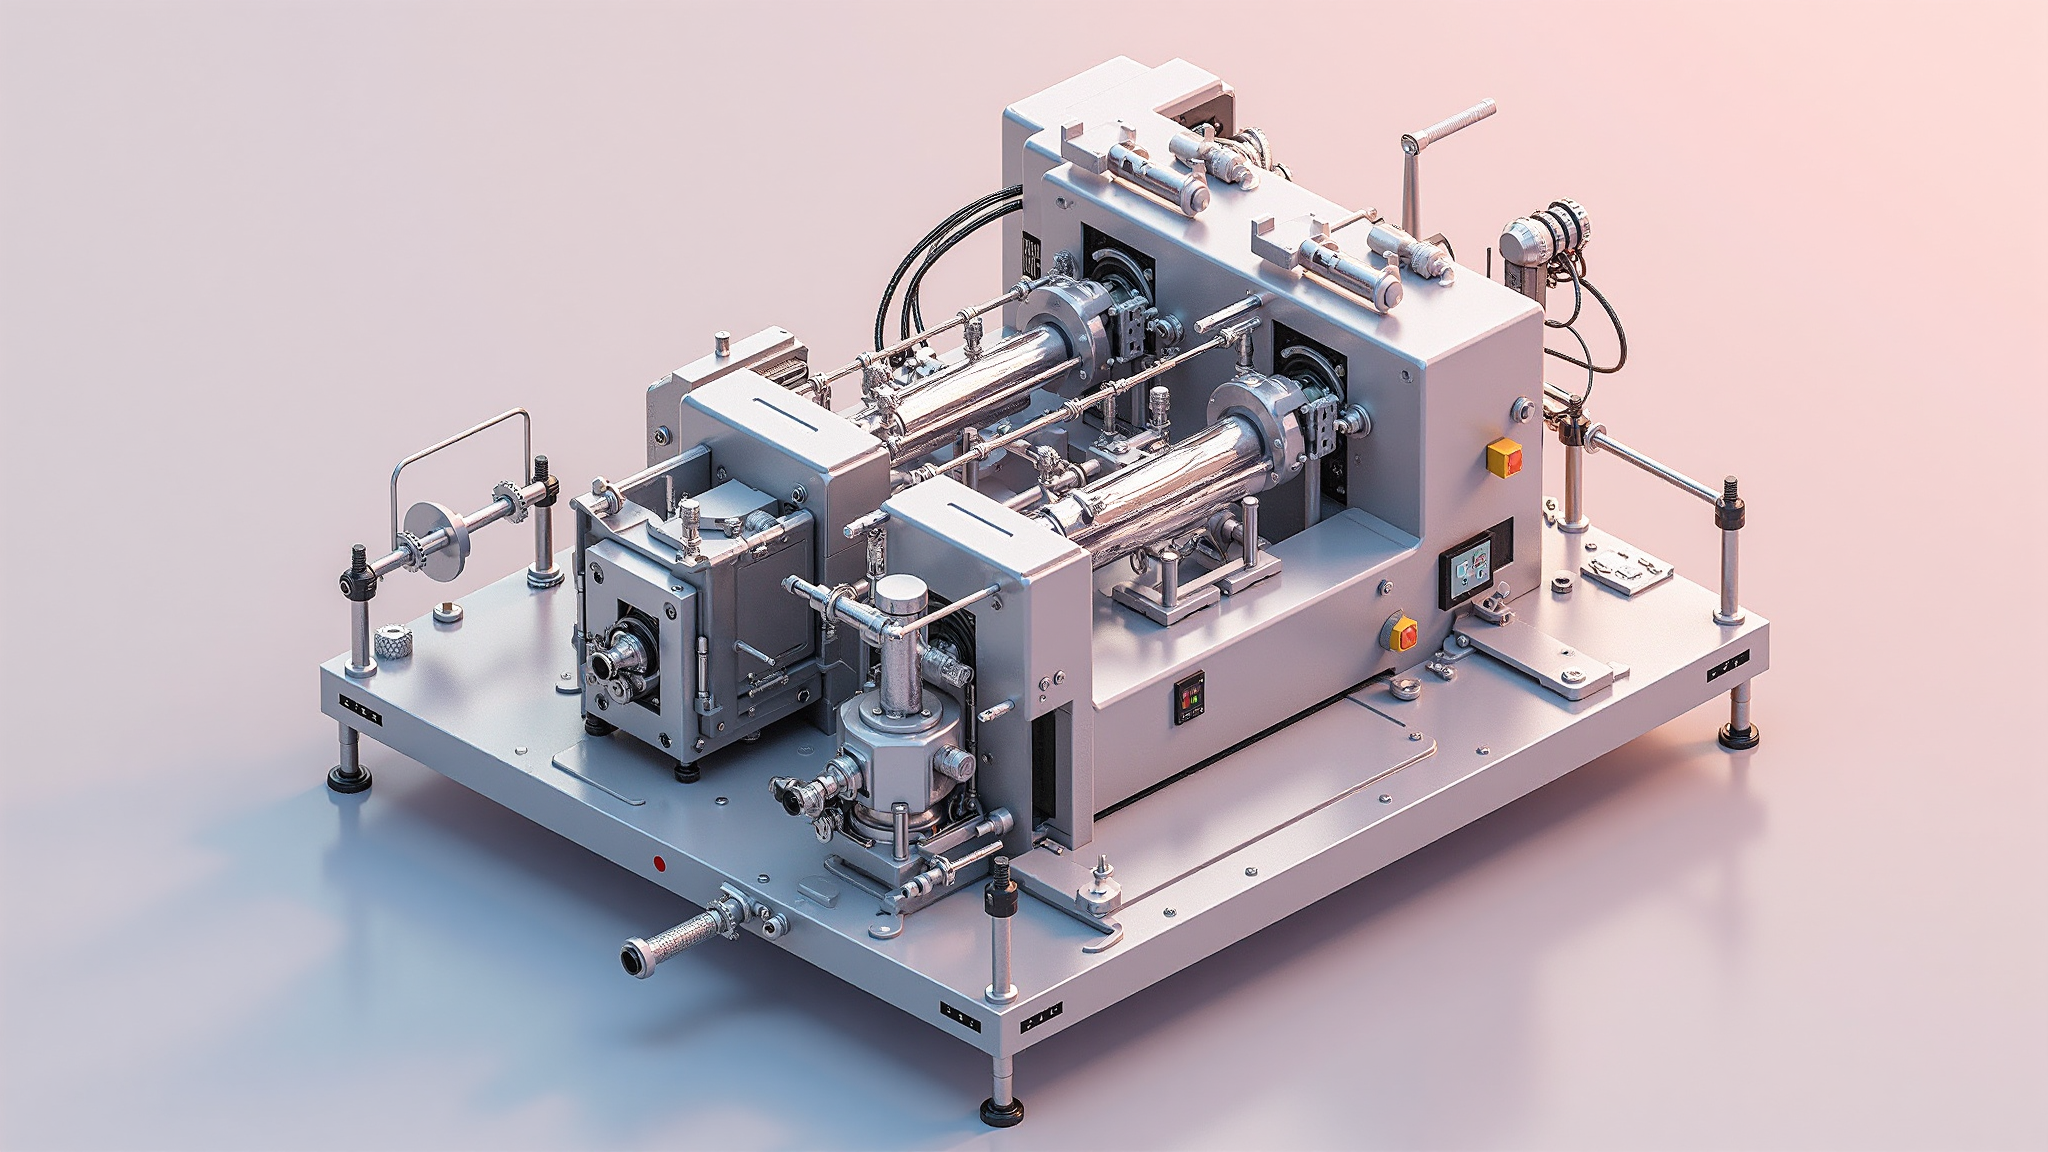
A gantry-type profile machining center for long aluminium and light-alloy extrusions. Typical 6 m stroke accommodates full-length window, curtain-wall and industrial frame profiles, with drilling, milling and sawing grouped on one long work table.
- CategoryProfile Machining Center
- 3 m profile, single spindle, standard tablePM-6500-3M
- 6 m profile with drilling and milling headPM-6500-6M
- 6 m with dual work zones and automatic profile clampsPM-6500-6MD
Price and lead time are quoted per configuration and quantity. Send us your part or capacity requirement and we will come back with a quotation.
Long-Stroke Gantry for Full-Length Profiles
The PM-6500 is laid out to machine extrusion profiles along their full length. A typical 6 m stroke covers standard architectural and industrial profiles, so drilling, milling and slotting are done on one long table instead of on several machines. Short 3 m versions are available for smaller sections.
Key Specifications Overview
| Item | Typical parameter |
|---|---|
| Machining length | 3000 / 6000 mm (optional) |
| X/Y/Z travels | 6500 × 500 × 300 mm (6 m version) |
| Spindle taper | BT30 / BT40 (selectable) |
| Spindle speed | up to 12000 r/min |
| Tool magazine | 8–16 stations |
| Positioning accuracy | approx. 0.05 mm |
| Clamping | pneumatic profile clamps along the table |
Profile Clamping and Work Zones
Pneumatic clamps run along the table so that a profile can be located without distortion, and the machine can be divided into two work zones to machine one profile while another is loaded. This keeps the spindle busy on long batch runs.
Milling, Drilling and Sawing Heads
Depending on the process, the machine can carry a milling head, a multi-spindle drilling head or a sawing unit. Grouping these operations reduces handling and keeps hole patterns and end cuts on the same datum.
Typical Part Families
Window and door profiles, curtain-wall mullions and transoms, solar mounting rails, industrial aluminium frames, and light-alloy structural extrusions that need repeated hole and slot patterns.
Configuration and Acceptance Points
Confirm the maximum profile length and section, the hole and slot patterns needed, and whether multi-spindle drilling or sawing is required. Acceptance typically includes a trial run of a representative profile and a check of hole position and end-cut squareness. Final configuration and quotation are subject to inquiry confirmation.
Need a Different Configuration?
Tell us the parts you machine and the batch size — we will recommend a machine or process that fits.